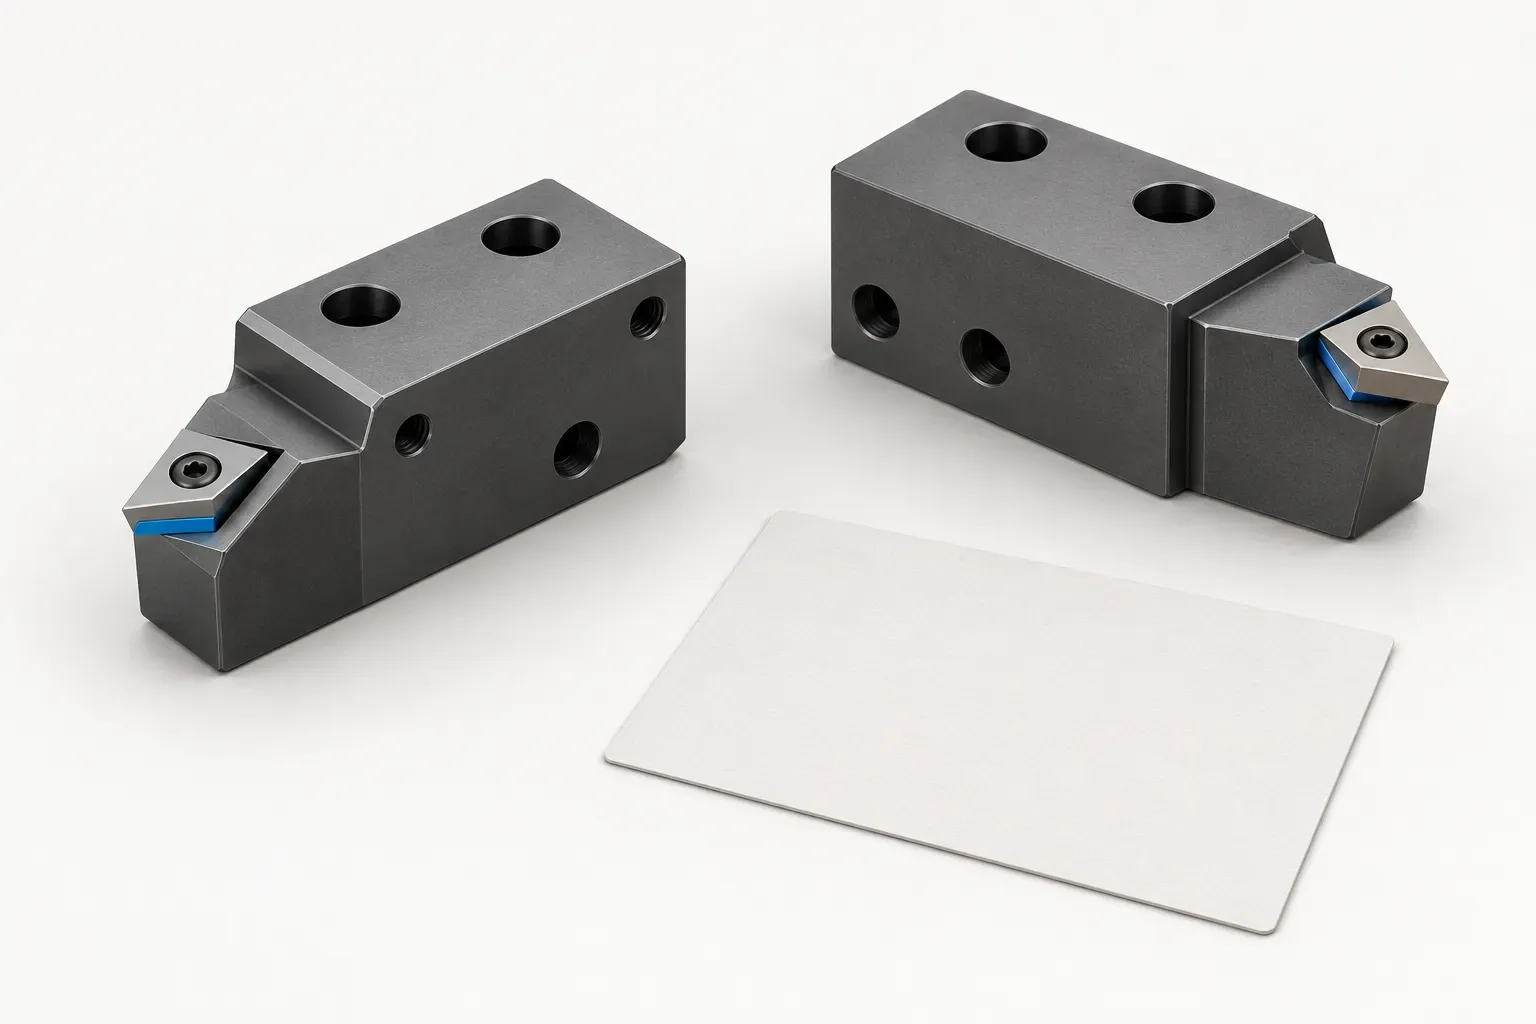
A CCMT1204 rough boring cartridge search can return sets for different system sizes and diameter ranges. The insert-family code is therefore not a complete set identity. Match the actual cartridge configuration to the head and intended working interval before using the family code to discuss inserts or replacement parts.
The documented examples below are useful when moving between larger boring configurations or checking a spare-part request. They share listed insert dimensions, but their connection designations, lengths and ranges differ. Those differences must remain visible rather than being collapsed into a single generic CCMT1204 product.
Identify the head and cartridge range together
Start with the head already selected or installed and record its exact identity. State the incoming feature, intended working diameter, bore depth, material and operation. A cartridge set should be evaluated against that assembly and requirement rather than selected solely from an insert stored in the workshop.
If replacing a set, provide the original cartridge identification and photographs showing its mounting position. Include the applicable head drawing where available. A partial code or familiar insert shape is a useful clue, but it does not resolve the component's locating geometry or its place in the assembly.
Compare the two documented CCMT1204 sets
The 95.0–116.0 mm cartridge set lists connection designation 36 and 74.0 mm overall length. The 115.0–136.0 mm cartridge set lists connection designation 46 and 96.5 mm overall length. Each record specifies two cartridges per set.
| Configuration field | First set | Second set |
|---|---|---|
| Boring diameter range | 95.0–116.0 mm | 115.0–136.0 mm |
| Connection designation | 36 | 46 |
| Overall length | 74.0 mm | 96.5 mm |
| Insert family | CCMT1204 | CCMT1204 |
| Cartridges per set | 2 | 2 |
Connection designations are system codes. They are not measured mounting diameters for the cartridges. The overlap between the two listed ranges does not prove interchangeability, common installation geometry or the ability to transfer one set to the other head.
Keep shared insert fields separate from cartridge geometry
Both records list an insert inscribed-circle diameter of 12.7 mm, an insert-hole diameter of 5.5 mm and a 12.9 mm cutting-edge length. Screw-on clamping is listed. These fields describe aspects of the documented insert seat; they do not make the supporting cartridges identical.
Neither example provides the complete grade and nose-radius suffix. Obtain the full insert specification needed for the workpiece and operation. Do not infer cutting conditions, material suitability, accuracy or a tool-life rating from the common family or insert dimensions.
The required fastening and setting instructions must also apply to the exact assembly. A shared insert family does not establish a common screw torque, allowable overhang or speed limit. Where the record is incomplete, request the applicable document rather than borrowing a number from another tool.
Do not extend a set to the entire head range
The 115.0–156.0 mm rough boring head lists a 46.0 mm pilot and working intervals of 115.0–136.0 mm and 135.0–156.0 mm using matching cartridges. The specific connection-46 set discussed above is listed for 115.0–136.0 mm.
Do not rewrite that set as covering 115.0–156.0 mm simply because the head's broad range reaches that value. The head and cartridge records describe different levels of the assembly. A requirement in another interval needs its own verified cutting configuration.
The shared system designation helps identify a candidate relationship, but the full drawings must establish the actual mating arrangement. Check locating features, orientation and fasteners, then review the complete installed envelope against the feature and access path. Cartridge overall length is not a guarantee of usable bore depth.
Specify the package and preserve the chosen configuration
Ask the quotation to identify the selected set, cartridges per set, mating head and required interval. State whether inserts, a shank, fasteners and other accessories are included in the request. Two cartridges per set does not prove that any particular insert quantity or accessory package is supplied.
Send the part drawing, material, bore depth, interface details and required quantity with the candidate identity. Clearly identify any missing installation or insert information that affects the purchase. The response should resolve those questions for the same configuration that was reviewed, rather than substitute a broad family description.
Retain the agreed component and insert records for future orders. This lets the next buyer reproduce the checked set without assuming that every rough boring cartridge carrying CCMT1204 is equivalent. The family narrows the search; the range, system identity and complete mating evidence establish the part being discussed.
Frequently asked questions
Are the connection-36 and connection-46 sets identical because both use CCMT1204?
No. They have different documented ranges and overall lengths. Shared insert-family fields do not prove cartridge interchangeability.
Does the 115.0–136.0 mm set cover the entire 115.0–156.0 mm head range?
No such coverage is established. The head lists separate intervals using matching cartridges; the specific set retains its own stated range.
Does two cartridges per set prove insert inclusion?
No. The quotation must identify inserts and accessories separately from the cartridge package.